Skip to Content
  • 4.0
    Impact Factor
  • 5.7
    CiteScore
  • 14 days
    Submission to First Decision
  • 3 days
    Acceptance to Publication

Journal of Manufacturing and Materials Processing

Journal of Manufacturing and Materials Processing is an international, peer-reviewed, open access journal on the scientific fundamentals and engineering methodologies of manufacturing and materials processing published monthly online by MDPI.

Get Alerted

Add your email address to receive forthcoming issues of this journal.

All Articles (2,064)

  • Article
  • Open Access

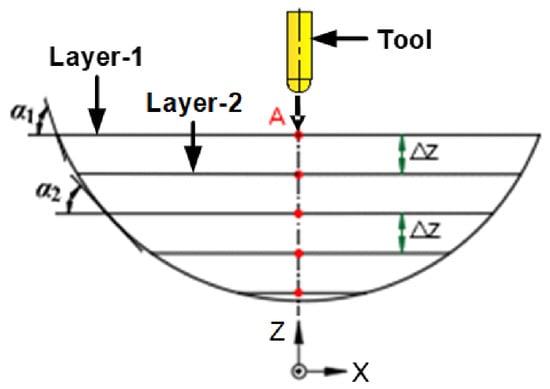
Incremental forming has great potential for flexible manufacturing of thin-walled parts. However, for ellipsoidal parts with varying curvatures, conventional constant layer spacing toolpaths easily cause local dents, excessive thinning and other defects. Existing helical toolpaths are designed for flat blanks and are poorly adaptable to curved blanks. An equal arc length spiral toolpath model for ellipsoidal parts was established, and simulations and experiments on flat and curved blanks were conducted to analyze wall thickness distribution and material flow behaviors. Results show that compared with two conventional toolpaths, the proposed toolpath achieves more balanced plastic flow, increasing the minimum wall thickness by 11.37% and reducing the maximum equivalent plastic strain by 7.03%, effectively alleviating forming defects at the ellipsoid bottom. This study verifies that the proposed toolpath and its composite forms adapt well to curved blanks, providing references for toolpath design of complex varying curvature parts.

Schematic of constant layer-spacing toolpath.
  • Article
  • Open Access

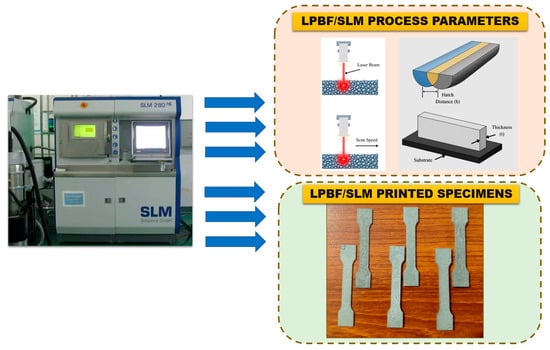
Laser powder bed fusion (LPBF) of AlSi10Mg alloy is highly sensitive to processing conditions, particularly when thin-walled components are fabricated. This study investigates the combined effects of wall thickness, laser power, scan speed, and hatch distance on the mechanical performance of LPBF-fabricated AlSi10Mg. A Box–Behnken design (BBD) based on response surface methodology was employed using 27 experimental runs. Wall thickness was varied from 1 to 3 mm, laser power from 320 to 380 W, scan speed from 730 to 1070 mm/s, and hatch distance from 80 to 130 μm. Relative density (RD), ultimate tensile strength (UTS), yield strength (YS), elongation at fracture, and hardness were evaluated as response variables. The statistical analysis showed that wall thickness and scan speed were the most influential factors for tensile properties, whereas the effects on RD, elongation, and hardness involved additional interaction and nonlinear terms. Among the developed models, the predictive performance is quite adequate along with comparatively higher fitted R2 values; however, only the RDrelative density model performance is limited by giving a negative predicted R2. Optimization of the four mechanical responses, excluding relative density, identified an exploratory candidate at 3.0 mm wall thickness, 320 W laser power, 1070 mm/s scan speed, and approximately 100.46 μm hatch distance. The corresponding predicted UTS, YS, elongation, and hardness were 354.7 MPa, 193.8 MPa, 13.54%, and 112.6 HV, respectively, with a composite desirability of 0.892. The results demonstrate the importance of considering component wall thickness together with LPBF process parameters when optimizing the overall mechanical performance of thin-walled AlSi10Mg components.

LPBF experimental system used for specimen fabrication and schematic representation of the investigated process parameters.
  • Article
  • Open Access

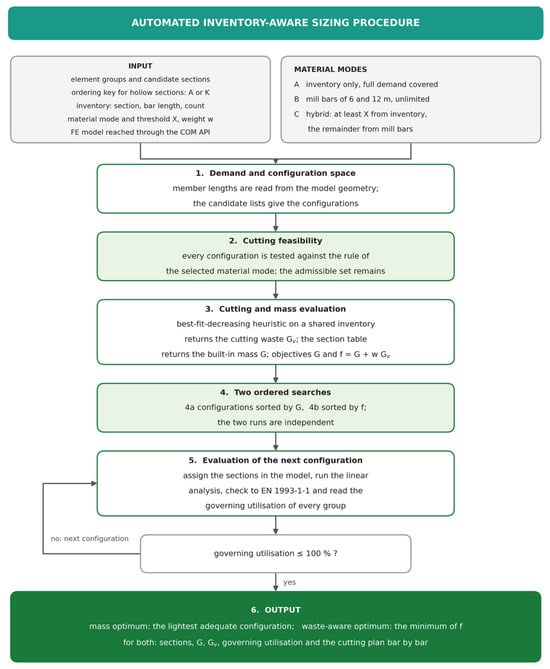
In steel construction, the material consumed comprises the mass built into the structure and the off-cuts left when members are cut to length. Sizing procedures minimize the first and disregard the second, assuming that the lightest structure also needs the least steel. This paper shows that the assumption can fail. An automated procedure is presented that drives an existing finite-element model through a programmatic interface, performs ultimate-limit-state member checks at every step, and evaluates the cutting of every configuration with a best-fit-decreasing heuristic on a shared inventory. Three material sources are covered: mill bars, a finite inventory, and a hybrid. The search returns the minimum-mass design and the minimum of a weighted objective that adds cutting waste to built-in mass. Exhaustive enumeration on two reference structures verified the search; an exact cutting check on the frame showed that the heuristic leaves the mass optimum unchanged but can alter the weighted optimum. On three benchmarks, a heavier but better-cuttable alternative used less steel than the statically lightest design by up to 1553 kg (9.2%). On a large hall, the hybrid mode lowered the built-in mass of the weighted inventory-only optimum by 4.4 t and raised governing utilization from 53% to 91%.

Flow chart of the sizing procedure.
  • Article
  • Open Access

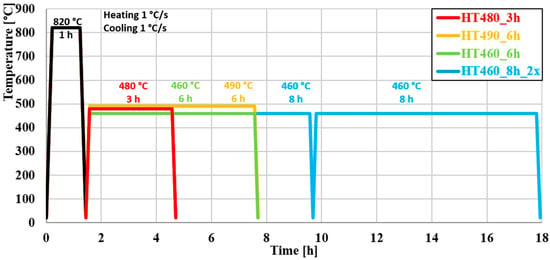
This study evaluates the effect of different precipitation-hardening regimes on the microstructure, hardness, and tribological behaviour of W720 maraging steel. Experimental specimens were aged at temperatures ranging from 460 to 490 °C for 3–16 h following solution annealing. Tribological tests were performed using the Ball-on-Flat method under dry sliding conditions against a G40 steel ball. The worn surfaces were analysed using LSCM, SEM, and EDS. Aging increased the hardness from 323 HV1 to 580–606 HV1 and reduced the coefficient of friction from approximately 0.75 to 0.63–0.71. The lowest nominal specimen wear volume was measured for the as-received, solution-annealed W720 condition (0.011 mm3), followed by HT490_6 (0.012 mm3); these values were compared descriptively without inferential statistical testing. However, the reference specimen produced a narrow, locally deepest wear track and caused the highest wear of the counter-body. The highest wear volume of the specimen was recorded for HT480_3 (0.027 mm3), while HT460_8x2 combined the highest hardness and the lowest coefficient of friction with a high wear volume. The dominant wear mechanism was a combination of abrasive grooving, adhesive damage, and tribo-oxidation. The results demonstrated that the tribological resistance of W720 is not governed by hardness alone, but rather by the interplay between microstructure, wear-track geometry, wear-product morphology, and the distribution of wear between the specimen and the counter-body.

Schematic representation of the heat-treatment cycles applied to the W720 samples.

Featured Articles of Last Quarter

Highly Accessed Articles

News & Conferences

Latest Issues

Open for Submission

Journal Sections

XFacebookLinkedIn
J. Manuf. Mater. Process. - ISSN 2504-4494